High Capacity Reverse Osmosis System for Industrial Use

By:Admin on 2025-03-13 03:11:23

Large Reverse Osmosis System: A Game-Changer in Water Purification TechnologyWater scarcity is a pressing global issue that affects millions of people every day. With the increasing pollution of natural water sources, finding sustainable and efficient water purification methods has become a crucial priority. In this endeavor, [company name] has been at the forefront of developing cutting-edge water purification technologies, and their latest innovation, the Large Reverse Osmosis System, promises to be a game-changer in the industry.[Company name] is a leading provider of water treatment solutions, with a strong focus on innovation and sustainability. Their mission is to provide access to clean, safe water for all, and they have been working tirelessly to develop advanced water purification systems that can meet the ever-growing demand for clean water.The Large Reverse Osmosis System is the result of years of research and development, and it represents a significant advancement in water purification technology. Reverse osmosis is a process that uses a semi-permeable membrane to remove impurities and contaminants from water, making it suitable for drinking and various industrial applications. The Large Reverse Osmosis System is capable of purifying large volumes of water, making it ideal for industrial and municipal use.One of the key features of this system is its efficiency. The reverse osmosis process is known for its high efficiency in removing impurities from water, and the Large Reverse Osmosis System takes this to the next level. It is capable of removing a wide range of contaminants, including heavy metals, chemicals, and microorganisms, ensuring that the purified water meets the highest quality standards.Moreover, the system is designed to be highly sustainable. It is equipped with advanced energy recovery technology, which significantly reduces its energy consumption, making it more environmentally friendly than traditional water purification methods. Additionally, the system is built to last, with durable components that require minimal maintenance, resulting in lower operational costs and a longer lifespan.The Large Reverse Osmosis System is also highly customizable, allowing it to be tailored to specific water quality requirements. This versatility makes it suitable for a wide range of applications, from municipal water treatment plants to industrial facilities, where the quality of water is a critical factor in their operations.In addition to its technological advancements, [Company name] is committed to providing comprehensive support and services for the Large Reverse Osmosis System. They offer expert consultancy and technical support to help their clients integrate the system into their operations seamlessly. Furthermore, they provide ongoing maintenance and monitoring services to ensure the system continues to perform at its best, delivering high-quality, purified water consistently.The arrival of the Large Reverse Osmosis System is a significant milestone for [Company name] and the water purification industry as a whole. It represents a step forward in the quest for sustainable and efficient water purification technologies, addressing the pressing need for clean water in an increasingly water-stressed world.In conclusion, the Large Reverse Osmosis System is a testament to [company name]'s dedication to advancing water purification technology and their commitment to providing access to clean, safe water for all. With its unparalleled efficiency, sustainability, and versatility, this system has the potential to make a significant impact on global water scarcity and contribute to a more sustainable future for generations to come.

Read More

Advanced Vacuum Emulsifying Reactor Technology for Efficient Processing

By:Admin on 2025-03-10 04:48:24

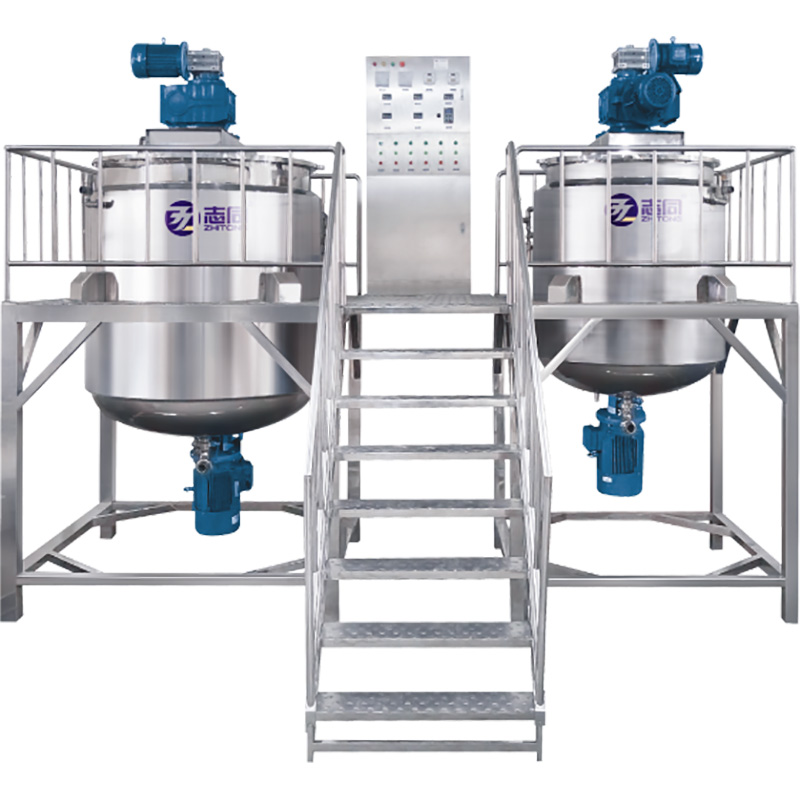
The Vacuum Emulsifying Reactor: Revolutionizing the Cosmetic and Pharmaceutical IndustryIn recent years, the cosmetic and pharmaceutical industry has seen a surge in demand for high-quality products that are not only effective but also safe for consumers. With this growing demand, manufacturers are constantly seeking innovative technologies to improve their production processes and ensure the quality of their products. One such technology that has been revolutionizing the industry is the Vacuum Emulsifying Reactor, a state-of-the-art machine that has been changing the game when it comes to emulsification, homogenization, and mixing in the production of cosmetics and pharmaceuticals.The Vacuum Emulsifying Reactor is a multi-functional machine that is designed to handle a wide range of processes, including mixing, homogenizing, emulsifying, and dispersing. It is an essential piece of equipment in the production of various products such as creams, lotions, gels, ointments, and other semi-solid or liquid products. What sets the Vacuum Emulsifying Reactor apart from other mixing equipment is its ability to perform these processes under vacuum conditions, which helps in reducing air bubbles and achieving a smoother and more stable product.This innovative technology has been gaining popularity in the industry due to its ability to significantly improve product quality, increase production efficiency, and reduce production costs. The Vacuum Emulsifying Reactor is equipped with advanced features such as a high-speed homogenizer, a scraping agitator, and a vacuum pump, allowing it to efficiently mix and emulsify even the most complex formulations. Its precise control system ensures that the desired product consistency and texture are achieved consistently, meeting the highest standards of quality and safety.In addition to its technical capabilities, the Vacuum Emulsifying Reactor also offers a high level of flexibility and customization, allowing manufacturers to adapt it to their specific production requirements. This means that it can be used for a wide range of products, from small-scale batches to large-scale production, making it an ideal solution for both small and large manufacturers in the cosmetic and pharmaceutical industry.One company that has been at the forefront of introducing and implementing the Vacuum Emulsifying Reactor in the industry is {}. With a strong focus on research and development, {} has been able to leverage the benefits of this advanced technology to provide its clients with high-quality, innovative, and customized solutions for their production needs. The company has been working closely with manufacturers to integrate the Vacuum Emulsifying Reactor into their production lines, helping them optimize their processes and achieve superior product quality.In addition to providing cutting-edge equipment, {} also offers comprehensive technical support and training to ensure that their clients are able to fully maximize the potential of the Vacuum Emulsifying Reactor. This includes assistance with installation, commissioning, and maintenance of the equipment, as well as training programs for operators and production staff to ensure smooth and efficient operation.The Vacuum Emulsifying Reactor has quickly become an indispensable tool for manufacturers in the cosmetic and pharmaceutical industry, setting new standards for product quality, production efficiency, and innovation. As the demand for high-quality and safe products continues to grow, the Vacuum Emulsifying Reactor is poised to play a crucial role in shaping the future of the industry, driving advancements in product development and manufacturing processes.With its exceptional performance, versatility, and reliability, the Vacuum Emulsifying Reactor is undoubtedly a game-changer for the cosmetic and pharmaceutical industry, and its impact will continue to be felt for years to come. As manufacturers continue to embrace this advanced technology, the industry is set to witness a new era of innovation and excellence in the production of cosmetics and pharmaceuticals. It is clear that the Vacuum Emulsifying Reactor has become an essential tool for manufacturers who are committed to delivering the highest quality products to their consumers.

Read More

Top Water Treatment Equipment for Your Needs

By:Admin on 2025-03-06 03:13:06

Water Treatment Equipment Company A, a leading provider of water treatment solutions, has recently introduced a new line of innovative water treatment equipment. The company, which has been at the forefront of the water treatment industry for over 20 years, has consistently pushed the boundaries of technology and design to deliver cutting-edge solutions for water purification and filtration.The newly introduced line of water treatment equipment is the result of extensive research and development, aimed at addressing the growing need for reliable and efficient water treatment solutions. With the increasing concerns over water quality and sustainability, the demand for advanced water treatment equipment has never been higher. Water Treatment Equipment Company A is committed to meeting this demand with their latest range of products, designed to deliver exceptional performance and efficiency.The new line of water treatment equipment includes advanced filtration systems, water softeners, reverse osmosis systems, and UV disinfection units. These products are engineered to deliver superior water quality, while also minimizing water wastage and energy consumption. The company has also incorporated smart technology into their equipment, allowing for remote monitoring and control to ensure optimal performance and efficiency.One of the key highlights of the new line of water treatment equipment is its modular design, which allows for easy customization and scalability. This flexibility is especially valuable for industrial and commercial applications, where water treatment needs can vary significantly. By offering modular solutions, Water Treatment Equipment Company A aims to provide tailored water treatment solutions that can adapt to the specific requirements of each customer.In addition to their focus on product innovation, Water Treatment Equipment Company A takes great pride in their commitment to sustainability. The company is dedicated to developing environmentally-friendly water treatment solutions that minimize the impact on the planet. Their new line of equipment incorporates eco-friendly materials and technologies, as well as energy-efficient operation to promote sustainable water treatment practices.Furthermore, Water Treatment Equipment Company A offers comprehensive support and services to ensure the successful implementation and maintenance of their water treatment equipment. Their team of experienced engineers and technicians are equipped to provide expert guidance and assistance throughout the entire lifecycle of the equipment, from installation to ongoing maintenance and support.With their new line of innovative water treatment equipment, Water Treatment Equipment Company A is poised to set a new benchmark in the industry. Their dedication to product excellence, sustainability, and customer satisfaction positions them as a trusted partner for water treatment solutions. As the demand for reliable and efficient water treatment equipment continues to grow, Water Treatment Equipment Company A is well-positioned to meet the needs of their customers and make a positive impact on the global water treatment industry.In conclusion, the introduction of the new line of water treatment equipment by Water Treatment Equipment Company A represents a significant milestone in the company's continued commitment to providing cutting-edge solutions for water purification and filtration. With their focus on innovation, sustainability, and customer satisfaction, the company is well-positioned to lead the way in the evolving water treatment industry. As the demand for advanced water treatment solutions continues to rise, Water Treatment Equipment Company A is poised to make a meaningful contribution to the global effort to ensure access to clean and sustainable water for all.

Read More